Finished component reference · drawing-based production
Deep-Bore Aluminum Die Cast Housing
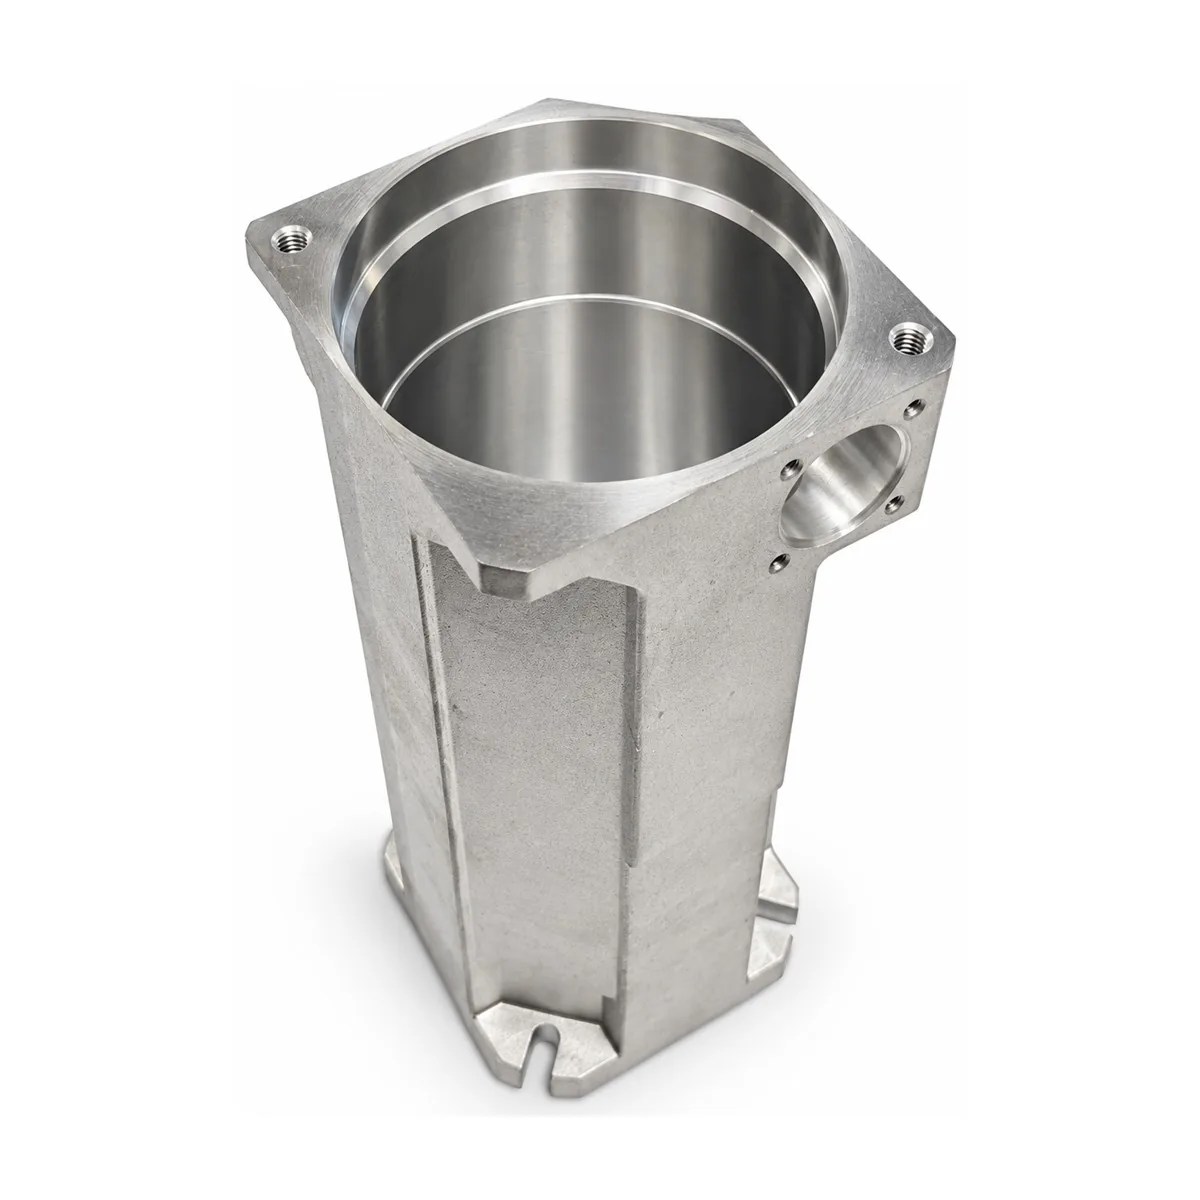
A tall reinforced casting with a deep machined bore, flange and side interface. Actuator, sensor, motor or mechanical module housings after the internal component stack and sealing function are defined.
 Aluminum alloy; exact grade confirmed by drawing and purchase specification
Photo-backed manufacturing evidence
Use the finished component as a reference, then control the new project from its drawing.
The photographs show a completed Huabo production example. They support discussion of comparable geometry, machining access and finish handling, but they do not define the alloy, dimensions, tolerances or performance limits for another project.
| Review area | What the photograph supports | What the current project must define |
|---|---|---|
| Finished-part evidence | A real completed component photographed after secondary operations | Current 3D model, controlled 2D drawing and revision |
| Geometry | A deep cylindrical cavity sits inside a tall tapered casting with reinforced outer walls, a mounting flange, local lugs and a side port. | Envelope, wall sections, draft, datums and controlled features |
| Application context | Actuator, sensor, motor or mechanical module housings after the internal component stack and sealing function are defined. | Assembly function, loads, exposure, interfaces and regulatory needs |
| Material basis | Aluminum alloy; exact grade confirmed by drawing and purchase specification | Required alloy standard, material certificate and approved alternatives |
| Production scope | DFM, tooling, high-pressure die casting, trimming and required secondary operations | Annual volume, validation level, surface finish, packaging and delivery requirements |
| Critical control | Control bore size and form at depth, axis position, flange flatness, side-port location, wall integrity and any specified sealing test. | Numeric acceptance limits, test method, sampling and report format |
Part-specific engineering review
The control plan follows the functional relationships visible in this geometry.
The points below are the practical issues to close during DFM, quotation and sample approval. The customer drawing remains the authority for every numeric limit.
Assembly role to confirm
Actuator, sensor, motor or mechanical module housings after the internal component stack and sealing function are defined.
Geometry and tooling focus
A deep cylindrical cavity sits inside a tall tapered casting with reinforced outer walls, a mounting flange, local lugs and a side port.
Machining and finish focus
Deep-bore access, cylindricity and axis-to-flange location must be planned with stable clamping and sufficient machining stock.
Inspection and release evidence
Control bore size and form at depth, axis position, flange flatness, side-port location, wall integrity and any specified sealing test.
Controlled production route
From drawing review to a repeatable finished component.
The final route is selected only after alloy, annual demand, tolerances, finish and validation requirements are known.
- Drawing and DFM reviewConfirm revision, functional datums, wall transitions, draft, parting, slides, machining stock and critical characteristics.
- Tooling and casting trialPlan filling, overflow, venting, cooling and ejection around functional and visible surfaces; record trial corrections before approval.
- Secondary operationsTrim, machine, deburr, clean and finish only to the controlled route, with fixtures transferring the agreed datum scheme.
- Inspection and releaseLink material records, first-piece results, appearance evidence and any functional test to the current drawing revision.
RFQ and validation package
Send the inputs that determine tooling, machining and inspection.
Provide a STEP or native 3D model together with the controlled 2D drawing. Include material standard, prototype and annual quantities, finish, assembly function, test conditions, documentation and packaging requirements.
For this component, identify: internal stack, bore depth and tolerances, flange datum, side-port function, sealing method and inspection access
A complete RFQ allows casting, machining, finishing and inspection to be quoted as one traceable scope. Assumptions should be listed before tool authorization.
Request a quotation for this component family.
Reference “Deep-Bore Aluminum Die Cast Housing” and attach the current drawing, annual demand, finish and quality requirements.