The selection answer
Zamak 3 is the safer default when a zinc die cast part needs a broad balance of castability, dimensional stability, ductility and finishing. Zamak 5 adds copper and is normally considered when higher tensile performance, hardness or creep resistance matters, but its lower ductility can be a disadvantage for bending, riveting, swaging or crimping after casting. The drawing should name an accepted alloy designation and standard rather than relying on “zinc alloy.”
The decision is not a contest between two catalogue numbers. It connects service load, temperature, wall geometry, joining operations, surface finish, dimensional risk and the material evidence required at approval. This guide gives engineering and purchasing teams a defensible way to compare Zamak 3 and Zamak 5 before a zinc die casting quotation is released.
Start with an alloy designation that both sides can verify
“Zamak” is a family name, not a complete purchase requirement. Alloy 3 and Alloy 5 also appear under regional designations such as ZP3/ZP5, ZnAl4/ZnAl4Cu1 and ZDC2/ZDC1. ASTM B86 lists Alloy 3 as AG 40A (UNS Z33525) and Alloy 5 as AC 41A (UNS Z35533). The applicable drawing or purchase order must state the system and edition that governs acceptance.
Do not translate a familiar trade name into a different standard by assumption. Chemical limits, test methods and acceptance language belong to the agreed specification. Ask the supplier to repeat the designation on the quotation, material certificate and first-article record. Huabo’s zinc die casting capability should be read together with the customer drawing, not as a replacement for it.
Zamak 3 and Zamak 5 trade ductility against added strength and hardness
The International Zinc Association describes Alloy 3 as the widely used reference alloy because of its balance of castability, long-term dimensional stability and finishing response. Alloy 5 contains about one percent copper; published guidance describes modestly higher strength and hardness and improved creep performance compared with Alloy 3, accompanied by lower ductility.
| Decision factor | Zamak 3 | Zamak 5 | Question for the drawing review |
|---|---|---|---|
| General use | Balanced default for many shapes and finishes | Selected when added mechanical margin is useful | Which property is actually controlling? |
| Ductility | Generally more forgiving | Lower than Alloy 3 | Will the part be bent, crimped, riveted or swaged? |
| Strength and hardness | Baseline for comparison | Moderately higher published values | Is the load case static, impact, wear or long-term? |
| Creep | Must be checked against time and temperature | Improved relative performance is often a selection reason | What deflection is allowed over the actual service life? |
| Finishing | Well established for plating and coatings | Also readily finished | What appearance, adhesion and corrosion test applies? |
Published specimen values are useful for screening; they are not a warranty for a production feature. Section thickness, porosity, temperature, load direction and aging affect the real part. Validate the requirement on the geometry and condition that will be delivered.
Let the service condition eliminate the wrong answer
Begin with the function. A decorative frame with snap features, a threaded fluid fitting and a loaded mounting bracket do not ask the material to do the same work. Record continuous and peak temperature, sustained load, impact, clamp force, vibration, environment and expected life. If long-term deformation controls the design, a room-temperature tensile table is not enough.
For a component near a heat source, ask for the allowed movement at the relevant time and temperature. For a fastened joint, define preload and bearing area. For a latch or post-formed feature, define the assembly strain and minimum ductility. The consumer-appliance application page, fluid-control components and industrial equipment examples show why one alloy sentence cannot cover every duty.
Geometry and die filling can matter more than the small property difference
Thin walls, long flow paths, isolated heavy sections, sharp transitions and deep cores change filling, solidification, ejection and dimensional behavior. Alloy choice cannot rescue a part whose flow path, draft, gate access or local mass is fundamentally unsuitable. Review alloy and geometry in the same DFM loop.
Mark cosmetic faces, pressure or sealing zones, threads, bearing surfaces and areas that will be machined. Decide whether a thread should be cast, tapped or formed with an insert. Place parting lines, overflows and ejector marks where they do not conflict with function. Huabo’s tooling and DFM route and guide to zinc die cast thread design explain these decisions in more detail.
Check every operation performed after casting
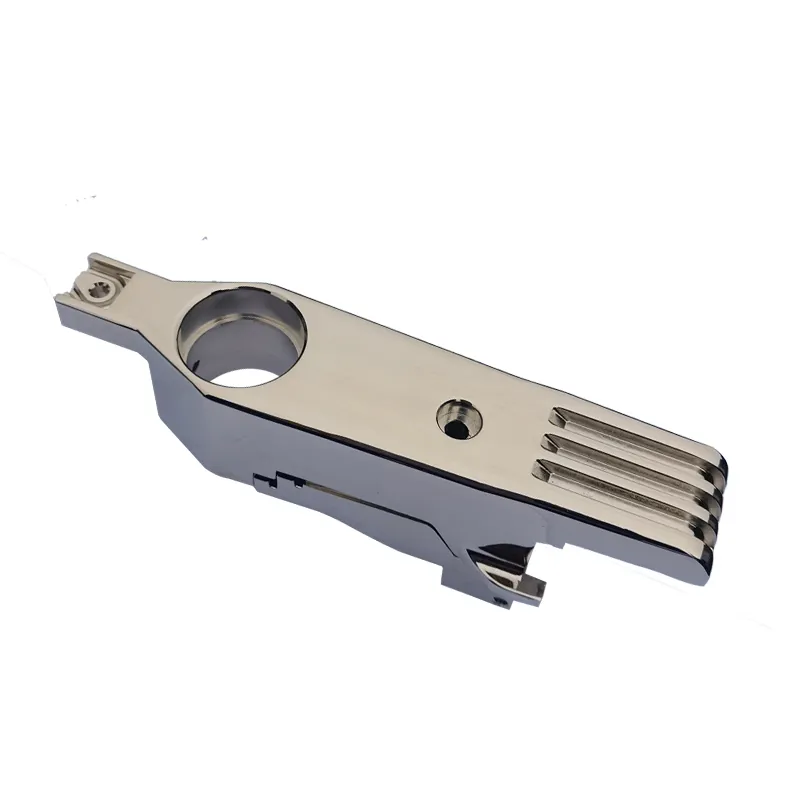
The alloy decision continues after ejection. Trimming, tumbling, drilling, tapping, machining, polishing, plating, painting, assembly and staking can expose different weaknesses. Alloy 5 may provide useful hardness, but its lower ductility can matter if tabs are bent or posts are swaged. A highly polished plated surface needs stable base-metal quality and a finishing process matched to the appearance class.
- Post-forming: identify bend radius, displacement and inspection method.
- Threads: define class, coating allowance, gauge and torque or pull-out requirement.
- Plating or coating: state appearance zones, thickness, adhesion and corrosion validation.
- Machining: protect datum strategy and avoid opening a critical surface without stock review.
- Assembly: define press fit, clamp load and any dissimilar-material corrosion concern.
Compare finishing options in the surface-finish selection guide and actual manufacturing scope on the zinc die cast product family.
Control the metal as a production input, not only as a label
Material identity depends on receiving control, furnace practice, segregation and traceable records. The approval package should identify the alloy specification, supplier or certificate reference, heat or melt trace where required, and the rule for return metal. A certificate is useful only when it can be connected to the production lot and the required chemical limits.
Define whether independent chemistry confirmation is required for first article, periodic verification or a risk event. Avoid writing a universal test frequency into a generic web guide: customer-specific, regulatory and product-safety requirements govern. The quality overview and inspection capability show how material evidence sits beside dimensional and functional results.
A threaded fitting and a decorative bracket lead to different alloy questions
Threaded fitting
The engineering review may prioritize thread integrity, local wall around the port, sealing face, plating allowance, torque and sustained load. Zamak 5 can enter the discussion if added hardness or mechanical margin is justified, but the final choice still depends on thread geometry, service temperature and validation. See the zinc hex male-thread fitting and hex threaded coupling as geometry references, not catalogue specifications.
Decorative or post-formed bracket
Surface quality, plating appearance, dimensional stability and a crimped or staked feature may favor the balanced ductility of Alloy 3. The production team still needs an approved surface standard and objective defect zones. The threaded mounting bracket illustrates how functional and cosmetic requirements can occupy the same component.
Put these alloy decisions into the RFQ before comparing prices
| RFQ field | Minimum usable statement | Why it changes the quotation |
|---|---|---|
| Alloy and standard | Exact designation, edition and approved equivalents | Sets chemistry and acceptance basis |
| Service condition | Load, temperature, life and environment | Prevents selection from room-temperature data alone |
| Post-casting work | Machining, forming, threads, finish and assembly | Changes ductility, stock and surface requirements |
| Critical zones | Datums, cosmetic faces, sealing and loaded features | Guides tool layout and inspection effort |
| Evidence | Certificate, first article, chemistry and test reports | Defines traceability and cost |
| Change control | No alloy or route change without approval | Protects the validated configuration |
Add these fields to the wider die casting RFQ checklist. A supplier can then quote the material, tooling, finishing and inspection route on the same technical basis.
Questions engineers ask about Zamak 3 and Zamak 5
Is Zamak 5 always the stronger and therefore better alloy?
No. It offers moderately higher published strength and hardness, but “better” depends on ductility, post-forming, service temperature, geometry, finish and cost. Choose against the controlled requirement.
Can a supplier substitute Zamak 3 for Zamak 5?
Only when the customer’s controlled drawing and change process allow it. Similar casting behavior does not make two alloy designations interchangeable in a validated product.
Does the alloy number guarantee plating quality?
No. Alloy selection is one input. Base-metal cleanliness, casting surface, preparation, plating chemistry, thickness and handling also control the result.
Should the drawing include every regional name?
It should include one unambiguous governing designation and any accepted cross-reference. A long list without stating precedence can create more ambiguity.
Primary technical references used for this guide
Use the current contract edition required by the customer. These sources support material screening; they do not replace part-specific engineering validation.
Technical review record
- Reviewer
- Huabo
- Reviewed
- 23 October 2026
- Evidence basis
- Huabo drawing-based zinc casting workflow; cited ASTM, IZA and NADCA sources
- Scope boundary
- Customer drawings, service calculations, specifications and approvals remain authoritative
- Review trigger
- Recheck after an alloy, load, temperature, geometry, finish, supplier or standard change
No universal alloy choice or property guarantee is assigned here. Production acceptance must follow the agreed material standard and part-specific validation.
Alloy and DFM review
Send the load case and secondary operations with the drawing.
Provide the controlled 2D/3D files, alloy standard, service temperature, joining method, critical dimensions, finish, annual demand and inspection evidence. Huabo can review the zinc die casting and tooling scope without substituting an unspecified alloy.